Beyond Run Hours: What Diaphragm Pump Monitoring Can Actually Tell You
Plan diaphragm pump condition monitoring around cycle counts, fluid delivery and leak detection, with a defined action for each signal.
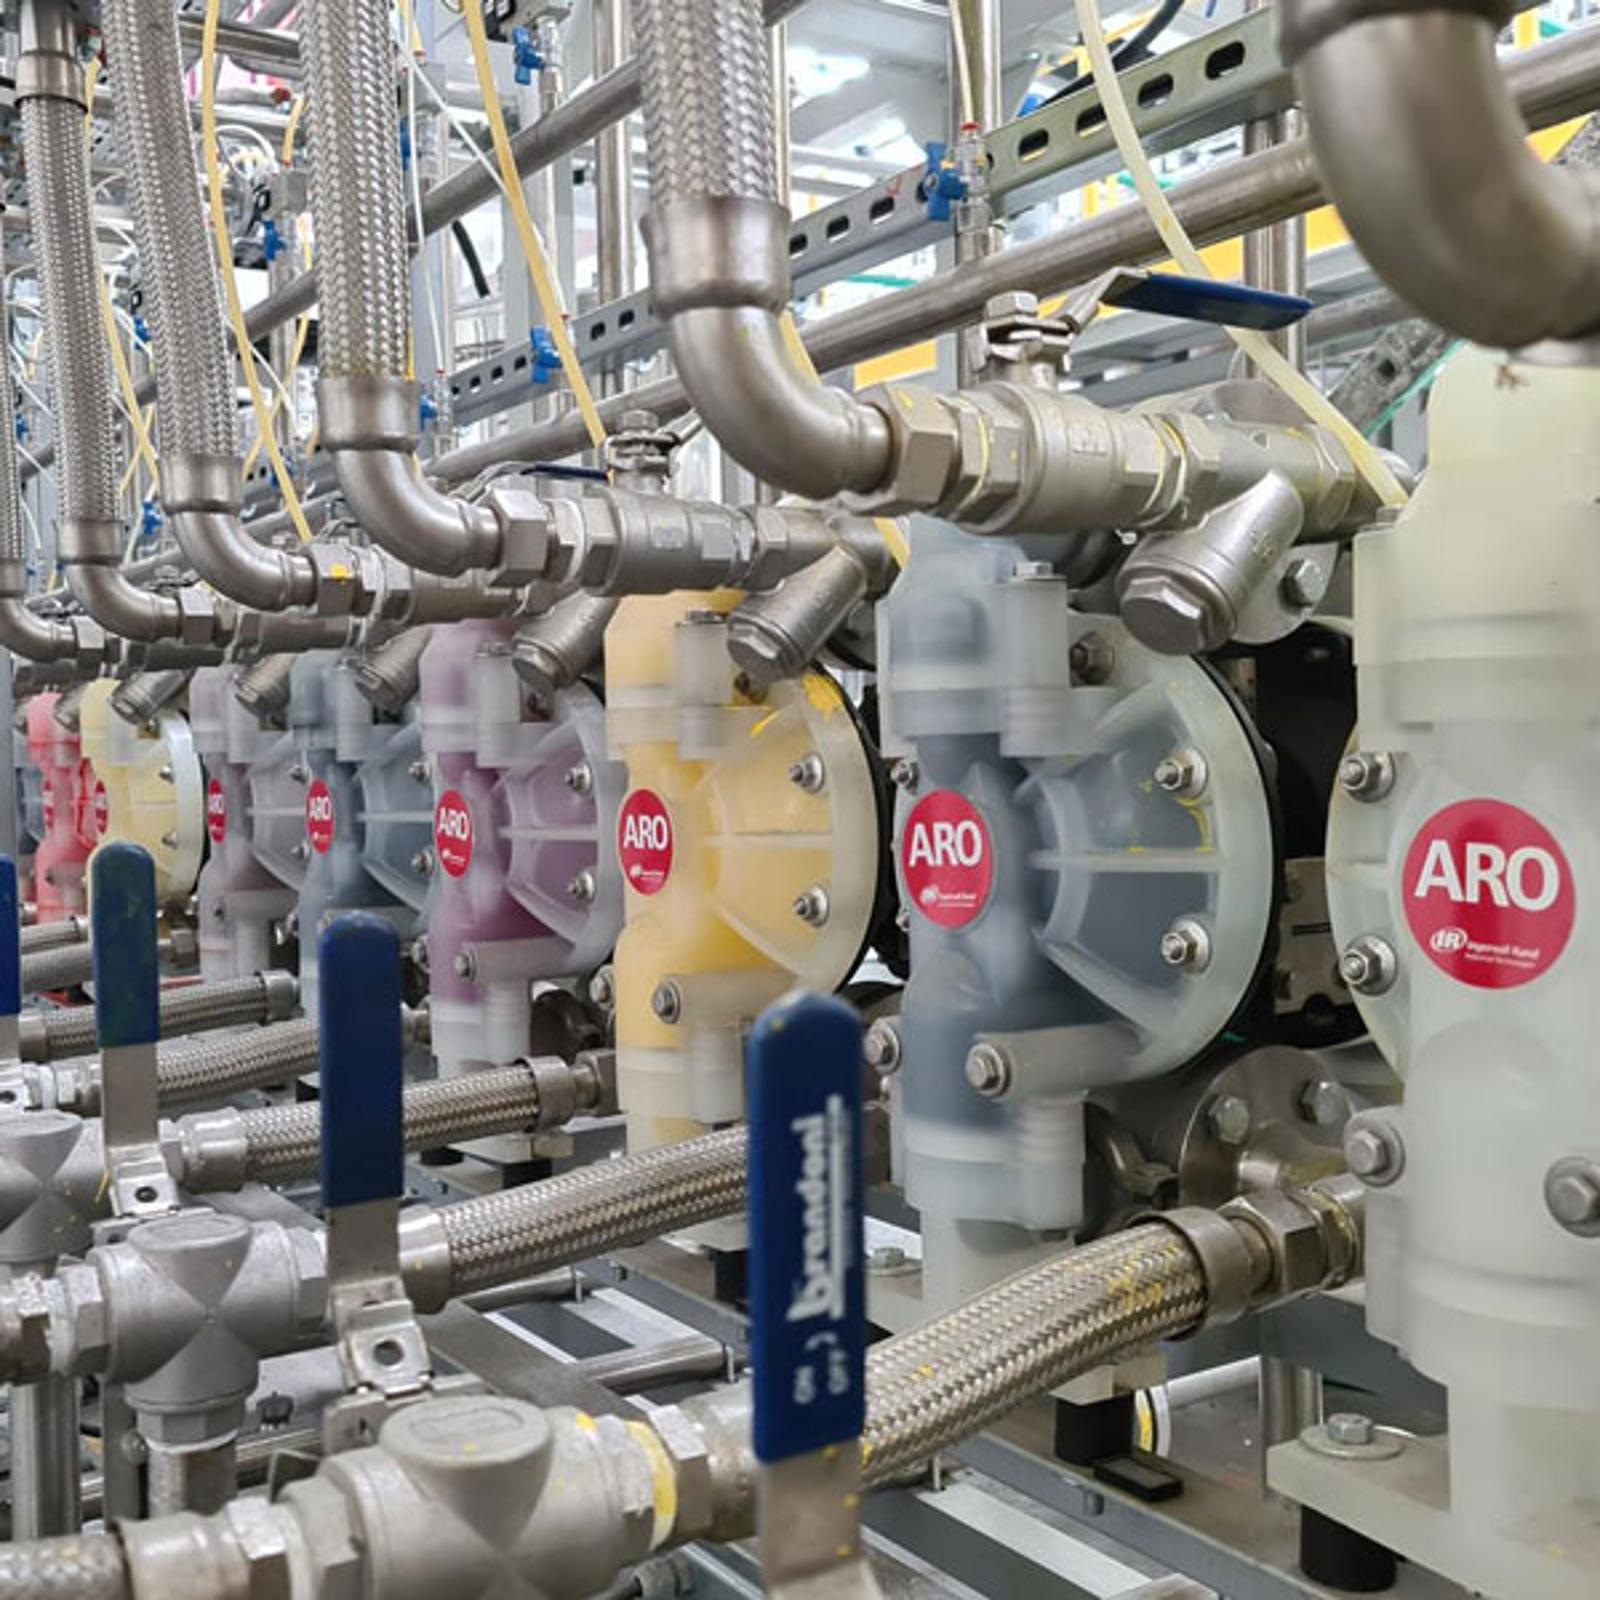
A pump that is cycling is not necessarily delivering the expected liquid volume. A pump that is stationary is not necessarily faulty. Those two distinctions are the starting point for useful diaphragm pump monitoring.
Practical diaphragm pump condition monitoring separates duty tracking from fluid-delivery measurement and failure indication. A diaphragm rupture detector can support leak detection on a compatible ARO diaphragm pump; it does not establish delivered volume.
Suppliers now offer several ways to add control and observation to pneumatic diaphragm installations. ARO's accessory portfolio includes level control, cycle-based batching, diaphragm-failure detection and over-run control. Each addresses a different question. Combining them without defining the operator response can produce more alarms without producing better decisions. [R4]
Diaphragm pump condition monitoring: define each signal
Cycle counting is useful for tracking duty exposure and comparing maintenance history. ARO's maintenance guidance specifically suggests tracking strokes between diaphragm replacements. That helps a plant move from “this pump failed again” to a record of how much work occurred before repair. It does not establish a universal replacement interval. [R5]
Liquid delivery needs different evidence. A cycle-based estimate depends on the effective liquid volume displaced per counted event. Priming, entrained gas, incomplete chamber filling and check-valve leakage can all change that relationship. First establish whether the counter reports a single stroke or a complete cycle; inconsistent terminology can create a two-to-one error before any hydraulic effect is considered.
| Signal | Useful interpretation | What it does not prove |
|---|---|---|
| Stroke or cycle count | Duty exposure and changes in cycling behavior | Accurate delivered volume without verification |
| Source-vessel level | Available liquid and an empty-vessel stop condition | That suction flow is unrestricted |
| Liquid in the air chamber | A diaphragm-failure warning on a compatible detection system | The root cause of the diaphragm failure |
| Air pressure near the pump | Available driving pressure during operation | Available air volume at every cycle rate |
| Measured fluid flow | Actual delivery at the measurement point | Product quality or material compatibility |
Build an operating-state record
A useful log distinguishes at least four states: stopped by command, priming, normal transfer and abnormal operation. Associate the signals with batch identity, fluid temperature and valve state wherever practical. A sudden rise in cycle rate during the final minutes of unloading may mean something very different from the same rise while the source tank is full.
For each alarm, define who acts, what is checked and whether restart is automatic or requires acknowledgment. If a leak detector trips, the response must address containment and the equipment's approved shutdown procedure. Resetting an alarm without investigating the fluid path can turn a warning into a repeated exposure.
Specify integration before ordering accessories
Confirm that the sensor or control accessory is approved for the pump model and intended environment. Record the required signal type, power supply, installation location and connection to the plant controls. A control that counts pneumatic cycles and a sensor that detects liquid in an air chamber are not substitutes for each other.
Also consider the failure state. What happens after loss of power, a damaged signal cable or loss of air? Who can restart the pump? These questions belong in the control description, alongside the normal sequence, rather than being resolved at commissioning.
Use monitoring to improve a maintenance decision
Begin with a small, measurable objective: identify empty-vessel running, document duty between repairs, or provide earlier notice of diaphragm failure. Record whether the added signal actually changes an action. If it does not, reconsider the threshold, the sensor location or the operating procedure before adding more instruments.
WILLEE enquiries can include the complete pump model, photographs of the air section and the intended control function. This makes it easier to distinguish a suitable accessory from a device that merely appears similar in a catalogue.
Prepare a pump-control enquiry
Technical references
[R4] ARO. Diaphragm Pump Controls.
[R5] ARO. AODD Pump Maintenance: 5 Key Tips for Longevity.
Application photographs are manufacturer reference images, not WILLEE customer-project claims. Model-specific instructions take precedence over this general engineering discussion.